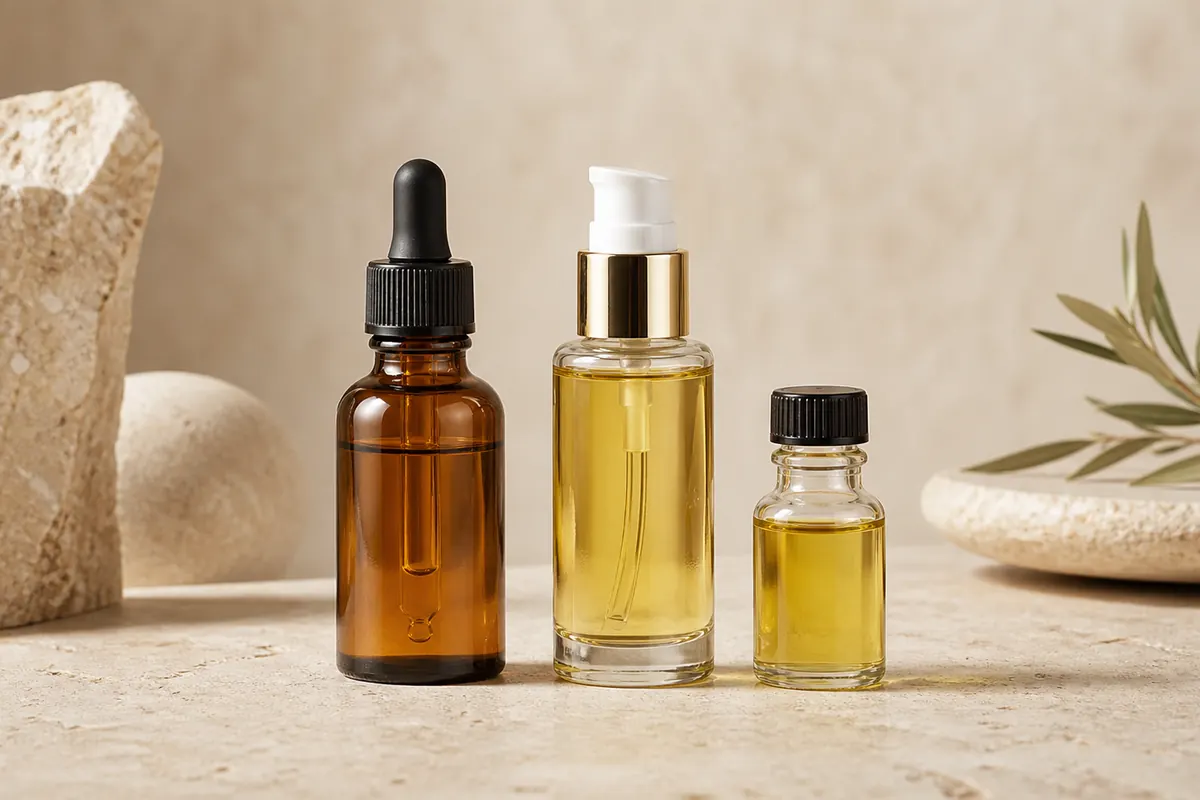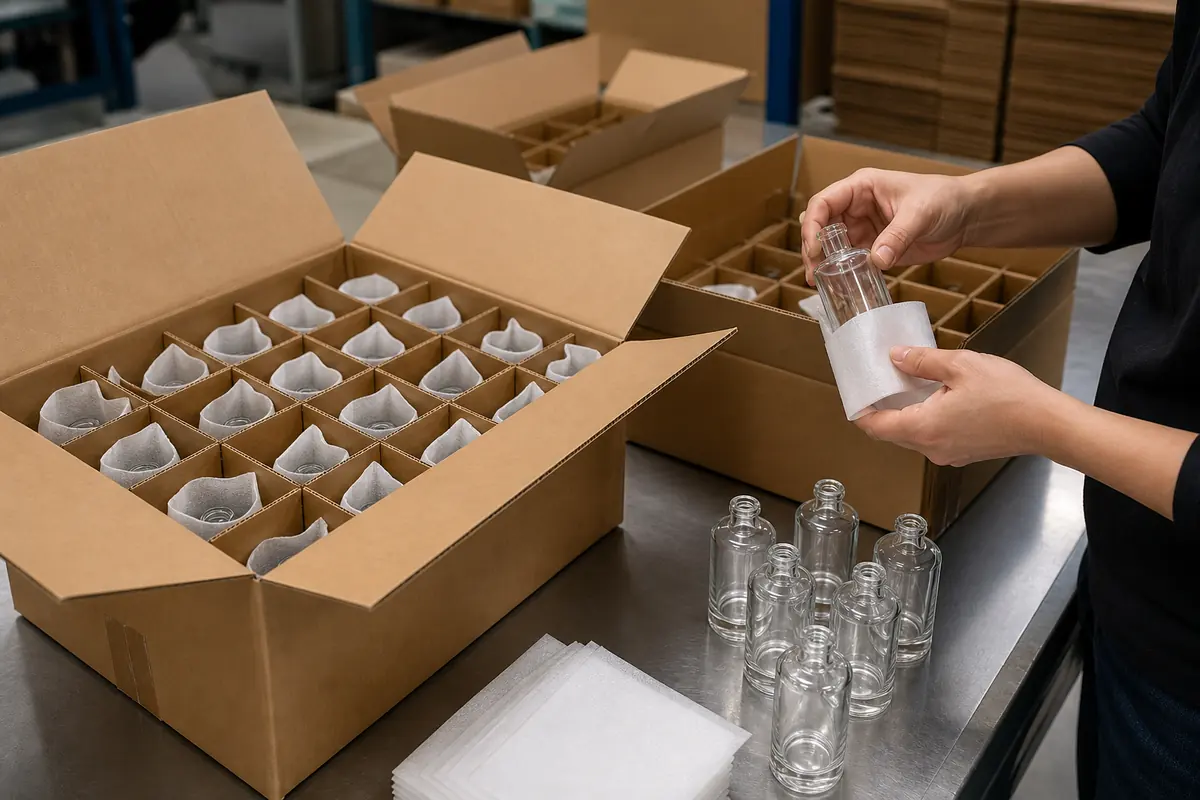
Refillable perfume packaging should be evaluated as a repeated-use system, not simply as a perfume bottle with a removable pump or cap. The bottle, refill interface, pump or closure, sealing components, fragrance formula, decoration, refill method and user sequence all affect whether the package continues to seal, spray and look acceptable after repeated handling.
For B2B buyers, the practical approval sequence is Refill Model → Bottle & Interface → Pump & Seals → Filled Compatibility → Refill Cycles → User Handling → Production Approval. This guide complements FOLOVER’s Packaging Applications resources and Packaging Buying Guides. Product-specific dimensions, neck or connection geometry, sealing materials, pump performance and compatibility should be confirmed from current drawings, supplier documentation and physical samples rather than inferred from a visually similar package.
The Core Buyer View: Refillability is a service model and repeated-use operating system
A removable pump or cap proves only that the package can be opened. Commercial refillability also depends on controlled transfer, repeatable resealing, component durability, error recovery, refill availability and a practical user journey. A technically refillable bottle can still be a weak commercial system if the user spills fragrance, cross-threads the closure, cannot identify the correct refill or gradually damages the sealing interface.
The sourcing question is therefore not simply “Can this bottle be refilled?” It is “Under which documented conditions does this complete refill system remain acceptable through its intended use?” That question produces clearer RFQs, better sample comparisons and more meaningful production approval.
| Refill Architecture | Best For | Main Advantage | Main Limitation | What Buyers Should Verify |
|---|---|---|---|---|
| User-opened threaded bottle | Projects where the primary bottle is intentionally opened and resealed for refilling | Relatively direct refill concept with fewer dedicated transfer components | Performance depends strongly on correct opening, resealing and closure engagement | Thread and sealing geometry, gasket condition, user handling, leakage and repeated closing performance |
| Dedicated valve or connector refill | Projects designed around a controlled refill-to-bottle connection | Can provide a more guided transfer path and reduce direct access to the bottle opening | Adds interface components, alignment requirements and supply-chain dependency | Connection geometry, shutoff behavior, venting, residue, misalignment and repeated connection cycles |
| Replaceable inner or cartridge | Systems where the durable outer pack remains while an internal fragrance container is replaced | Separates refill replacement from some of the primary bottle hardware | Adds fit, retention, identification and component-coordination requirements | Cartridge retention, compatibility, replacement sequence, SKU control and complete assembled fit |
Define what refillable means for the project
Refillable can mean that the consumer opens the primary bottle, connects a dedicated refill, replaces an inner container or participates in a return-and-reuse service. These are not equivalent packaging systems. Buyers should define who performs the refill, where it takes place, which component is opened or replaced, how many cycles the project intends to support, and how the user identifies the correct refill. FOLOVER’s refillable perfume packaging guide provides the corresponding A-page for bottle and sourcing decisions.
Current standards and regulation also treat reuse as more than a removable component. ISO 18603:2013, Packaging and the environment — Reuse, sets requirements for packaging to be classified as reusable and includes the associated reuse system. In the EU, Regulation (EU) 2025/40 separately defines concepts such as refill, rotation and re-use systems. For a packaging buyer, the implication is practical: “refillable” should describe a defined operating model, not merely an opening feature.
Before requesting samples, map the full journey from the empty or partially used bottle to the refilled, resealed and ready-to-use pack. Identify the components touched by the consumer or service operator, the intended fragrance formula, storage conditions and the acceptance evidence required after repeated use.
Choose the refill interface as a controlled connection
The refill interface controls how fragrance moves from the refill source into the primary package. A screw opening, dedicated valve connection or replaceable cartridge can each work, but each creates different sealing, venting and handling requirements. The interface should be selected together with the primary bottle and dispensing architecture, not added after the bottle design is already frozen. Buyers can also use the broader perfume packaging guide when bottle shape, closure and decoration decisions are being coordinated.
The most revealing failures usually appear outside the ideal demonstration: incomplete engagement, tilted connection, trapped liquid, incorrect orientation, overfilling or a user trying to force incompatible parts together. Sample evaluation should therefore include normal use plus foreseeable handling errors. The aim is not to make misuse impossible, but to identify which mistakes create leakage, contamination, difficult recovery or component damage.
For purchasing, request controlled drawings and material information for critical interface parts and establish which supplier owns each mating dimension. Similar-looking connectors should not be treated as interchangeable unless the selected components have been physically assembled and evaluated together.
Design the pump for removal or repeated connection
A perfume pump designed for one-time crimp assembly is not automatically suitable for a refill system that requires repeated removal. Threaded, cartridge-based or purpose-designed refill assemblies introduce different requirements for pump retention, sealing, gasket compression, collar alignment, actuator protection and repeated engagement. Buyers can review FOLOVER’s refillable perfume bottles when shortlisting packaging architectures.
A frequent sourcing shortcut is to keep the conventional bottle and pump and modify only the opening method. That can create a package that opens successfully but does not maintain sealing or spray performance after repeated assembly. The bottle, pump, closure structure, gasket or sealing element, collar and dip tube should therefore be approved as one assembly.
Where atomization is part of the final system, spray performance should also be checked after refill and reassembly rather than only on the original filled sample. The related guide on how perfume atomizers work explains the relationship between the bottle, pump and spray system in more detail.

Manufacturer Insight: From a packaging manufacturing perspective, a nominally similar neck or threaded connection is not enough to establish compatibility. Bottle finish, thread geometry, sealing surface, gasket structure, pump construction, collar and assembly sequence can all affect the result. Final bottle and closure compatibility should be confirmed using the selected components and physical samples before bulk production.
Treat every seal as a wear component
Repeated opening and refilling can change the condition of gaskets, liners, valves and other sealing surfaces. Compression set, abrasion, fragrance residue, contamination or incorrect reassembly may alter performance even when the first filled sample passes a basic leak check. Buyers should identify every sealing interface and determine which ones are disturbed during a refill cycle.
For continuous-thread closures, ASTM D2063/D2063M-24 provides a method for measuring removal-torque retention of container and continuous-thread closure systems under predetermined conditions. It does not provide one universal torque value for refillable perfume packaging. Application and removal criteria still need to be established for the actual bottle, closure and sealing structure.
Do not approve a refill system only from a new assembly. Inspect the seal and closure after the intended refill sequence, storage and repeated opening. If a gasket, liner, valve, neck finish or closure supplier changes, determine whether revalidation is required before assuming equivalent performance.
Failure mode to watch: A closure can still feel tight while the sealing surface is contaminated, compressed differently or partially damaged. User feel is useful, but it should not replace filled-package leakage and compatibility evaluation.
Control transfer loss and residual fragrance
Refill performance is not only about nominal refill volume. Fragrance can remain in the refill container, connector, valve, dip tube or other dead spaces, while external residue can be created during disconnection. These losses affect user experience, cleanliness and any commercial claim about how efficiently the refill is transferred.
Instead of guessing an acceptable loss percentage, define a project-specific evaluation. Record the mass or amount supplied for the test, the amount successfully transferred, visible external residue and liquid that remains inaccessible after the refill sequence. Compare the same package architecture using the same formula and procedure.
Headspace also matters because the user may refill a bottle before it is completely empty. Test the actual intended refill sequence rather than only filling an empty bottle under controlled factory conditions. Packaging compatibility should be evaluated with the actual formulation under intended storage and use conditions.
Design for user error and recovery
Consumers may cross-thread a closure, refill too quickly, tilt the bottle, overfill it or reconnect a pump incorrectly. A robust refill system should make the correct sequence understandable and reduce the consequence of foreseeable mistakes. Visual cues, orientation, grip, stop features, component asymmetry and instructions can all influence whether the user completes the process correctly. Buyers considering the broader bottle architecture can also review how to choose a perfume bottle.
Testing only a trained operator can hide these problems. After the basic engineering check, observe uncoached or minimally instructed use and intentionally evaluate realistic mistakes that the design is expected to tolerate. Record what happens when the sequence is interrupted or a component is only partially engaged.
For B2B approval, distinguish between an error that is merely inconvenient and one that can create leakage, fragrance contamination, permanent component damage or an unusable pack. The second group should be addressed before mass production rather than left to user instructions alone.
Verify decoration and appearance over repeated handling
A refillable primary bottle is intended to remain in use longer than a single-use pack, so its coating, printing, hot stamping, collar finish and cap surfaces can experience more handling and more opportunities for fragrance contact. Appearance should therefore be evaluated after relevant handling and filled-package use, not only on a freshly decorated empty sample.
Alcohol-containing fragrance or product residue can contact the neck, collar or bottle surface during spraying and refilling. Buyers should not assume that a decoration suitable for one formula or bottle will automatically perform the same way on another configuration. Final color, logo, coating and decoration should be approved using physical samples.
FOLOVER’s decoration and finishing page covers coating, frosting, screen printing, hot stamping and related finishing options. For a refillable project, decoration approval should be tied to the actual bottle and component configuration used for production.
Manufacturer Insight: At FOLOVER, we normally recommend approving decoration after the bottle and component system has been selected. Changing the collar, cap, coating or printed area after functional approval can create a new appearance or assembly variable that should be checked on physical samples.
Plan refill operations and supply continuity
A refillable packaging promise depends on the continued availability of the correct refill unit and compatible components. Similar connectors, caps or pumps may use different internal sealing structures or dimensions, so SKU identification and component revision control should be part of the packaging specification. Buyers can also review whether perfume bottles can be refilled for the shorter buyer-facing explanation.
The purchasing team should determine who controls the refill unit, primary bottle, pump, closure and decoration specifications; how changes are communicated; and whether a later component revision remains backward-compatible with packs already in the market. A durable glass bottle has limited commercial value as a refill platform if the corresponding refill or replacement component becomes unavailable.
Distribution requirements also belong in the project brief. Fragrance transport classification depends on the actual formulation and applicable transport mode and route. As one regulatory example, the U.S. Pipeline and Hazardous Materials Safety Administration explains that use of the “UN1266, Perfumery products” description depends on the product’s primary function and applicable hazardous-material classification. Buyers should therefore confirm transport requirements using the actual product information rather than copying another fragrance project’s shipping classification. See the PHMSA interpretation on perfumery products.
Evaluate environmental claims with evidence
A refillable perfume system may reduce the amount of primary packaging required for repeated product use, but that result is not automatic. The durable bottle can require more material, while refill packs, extra connectors, transport, cleaning, breakage and the number of refills actually completed can change the overall result. Buyers should therefore separate a verified design feature such as “refillable” from a broader claim such as “lower environmental impact.”
If a project makes comparative environmental claims, define the comparison boundary and assumptions. ISO 14040:2006 provides the principles and framework for life-cycle assessment, including goal and scope definition, inventory analysis, impact assessment and interpretation. The standard does not establish that refillable packaging is automatically preferable; the result depends on the actual system being assessed.
For procurement, useful inputs can include the mass and material of the primary package and refill, expected and actual refill behavior, transport assumptions and end-of-life route. Where evidence is incomplete, describe the verified refill feature without turning it into an unsupported absolute sustainability claim. The related article on why refillable beauty packaging is growing discusses the broader opportunities and trade-offs.

Approve the system across its intended life
Final approval should cover the package as it will actually be used: the initial filled pack, refill operation, repeated opening or connection, storage between uses, distribution and foreseeable handling errors. The retained approval sample should represent the complete bottle, refill interface, pump or closure, sealing parts, cap and decoration.
Do not create one universal test value simply because the package is refillable. Cycle count, storage duration, temperature conditions, leakage criteria, acceptable transfer loss and user-force limits should be defined from the actual project requirements and supported by the component suppliers, filler and brand quality team where appropriate.
The final production record should identify the approved component versions, formula used for compatibility evaluation, key drawings and the physical reference sample. Final bottle and closure compatibility should be confirmed using the selected components and physical samples before bulk production. Packaging compatibility should be evaluated with the actual formulation under intended storage and use conditions.
Manufacturer Insight: For a refillable perfume project, FOLOVER recommends locking the complete assembly before bulk production rather than approving the bottle, pump, cap and refill interface separately. This is particularly important when components are sourced or decorated by different parties.
Buyer Approval Checklist
- Define exactly how and where the perfume will be refilled and who performs the operation.
- Identify the primary bottle, refill container, interface, pump or closure, sealing components, cap and decoration in the approved configuration.
- Request current drawings and material information for critical mating and formula-contact components.
- Confirm which supplier controls each interface dimension and how component changes will be communicated.
- Evaluate production-intent samples rather than combining unverified parts from different sources.
- Test the intended or representative fragrance formula in the complete filled assembly.
- Evaluate leakage, resealing, spray performance, transfer loss, residual fragrance and component condition through the intended refill sequence.
- Include foreseeable user errors such as incomplete engagement, cross-threading, overfilling or incorrect reassembly where relevant to the design.
- Approve physical decoration samples after relevant formula exposure, handling and repeated-use evaluation.
- Review distribution requirements using the actual formula, transport mode and destination rather than assuming another perfume’s classification applies.
- Retain the approved physical assembly and establish revalidation triggers for critical material, component, supplier or process changes.
How to Structure the Sample Evaluation
Begin with a screening round that compares plausible refill architectures and complete component combinations. At this stage, remove options with obvious fit, connection, leakage, transfer, spray or handling problems. A successful short screening test is useful for eliminating weak options, but it should not be presented as proof of long-term performance.
Move the strongest candidates into filled evaluation using the intended or representative fragrance formula and production-intent components. Record the formula batch, bottle and component identities, assembly condition, refill sequence and inspection dates. The purpose is to make the result reproducible rather than to create an isolated demonstration sample.
At each inspection point, record objective observations and the buyer implication. Depending on the project, this can include leakage, package mass, closure condition, pump function, spray behavior, transferred fragrance, external residue, inaccessible product, decoration condition and user handling. If a result is close to an acceptance limit, investigate the mechanism and component tolerance before increasing order quantity.
Do not average away a serious outlier without understanding why it occurred. A single abnormal assembly can reveal dimensional variation, an incorrect component, assembly error or a failure mode that becomes more important at production scale.
Frequently Asked Questions
Can packaging be approved from an empty sample?
An empty sample can confirm appearance, basic fit, opening sequence and handling, but it cannot establish fragrance compatibility, long-term sealing, transfer behavior, spray performance after refilling or decoration durability. Final approval should use the intended or representative formula with the selected production-intent assembly under documented conditions.
Is a supplier’s standard component specification enough?
No. It is an important starting point, but refillable perfume performance depends on the exact bottle, interface, pump or closure, sealing materials, fragrance formula, assembly process and use conditions. Supplier specifications should define what then needs to be verified on the complete package.
What should trigger revalidation?
Changes to the fragrance formula, formula-contact material, critical bottle or interface dimensions, pump, gasket, closure, supplier, tooling, decoration or assembly process can affect performance. The project team should define which changes require partial or full revalidation before bulk production.
How should buyers compare two visually similar packages?
Compare controlled drawings, materials, sealing architecture, refill interface, pump configuration, assembled samples, filled test observations, user operation and change-control requirements. Similar appearance does not establish equivalent sealing, spray or refill performance.
Is a screw-openable perfume bottle automatically refillable?
No. A removable threaded closure only shows that the bottle can be opened. A commercial refill system also needs a controlled refill method, reliable resealing, compatible formula-contact components, repeated-use durability and a practical user sequence. Buyers should approve the complete refill architecture rather than the opening feature alone.
Should refillable perfume packaging be tested with the actual fragrance formula?
Yes. Fragrance composition can affect formula-contact components, sealing and decoration, and the refill operation can introduce conditions that are not visible in an empty fit check. Packaging compatibility should be evaluated with the actual or representative formulation under intended storage and use conditions before bulk production.
Conclusion
Refillable perfume packaging works only when the bottle, refill interface, pump or closure, seals, formula, decoration and user sequence remain compatible as one repeated-use system. A package that opens successfully once is not enough; the buyer needs evidence that it can be refilled, resealed, handled and used under the intended project conditions.
For B2B sourcing, define the refill model first, then approve production-intent components with the representative fragrance formula. Keep the successful physical assembly as the reference for bulk production and require review when a critical component, material, supplier or process changes.